High-Efficiency Generator Sets & Pneumatic Support Machinery
Explore heavy-duty prime power and industrial auxiliary machinery configured to keep critical pneumatic lines, compressed air stations, and manufacturing facilities running without downtime.
Engineering Superiority: Atlas Compatible Spare Parts & Fluid Engineering
In modern industrial air compression systems, balancing life-cycle maintenance cost with thermodynamic efficiency is paramount. Discover how precision aftermarket manufacturing provides 100% operational parity at a fraction of capital expenditure.
Screw Airend Overhaul & Dynamic Tolerances
The heart of any Atlas Copco GA, GX, or GR series compressor is the asymmetric helical screw airend. Our Chinese precision manufacturing centers employ Klingelnberg rotor grinding machinery delivering micrometer-level rotor profile accuracy, preventing air slippage, volumetric loss, and internal thermal cavitation.
High-grade German SKF and FAG angular contact ball bearings and cylindrical roller bearings are pre-loaded to counteract axial thrust, giving rebuilt or replacement air ends an operational MTBF (Mean Time Between Failures) exceeding 40,000 running hours under full continuous industrial load.
Multi-Stage Filtration & Micro-Separation
Particulate contamination degrades air quality, accelerates screw rotor wear, and damages pneumatic valves. Our alternative air intake filters use multi-density synthetic micro-glass media from HV (Hollingsworth & Vose), capturing 99.9% of particles down to 1-3 microns.
Furthermore, air-oil separators feature high-permeability borosilicate microfiber depth filters that maintain differential pressure below 0.2 bar (2.9 psi) throughout their 4,000-hour life cycle, limiting carryover to less than 3 ppm while conserving electric power in large rotary networks.
Valves, Sensors & Thermodynamic Regulation
Proper air delivery requires precision pressure regulation and temperature control. We manufacture replacement minimum pressure valves (MPV), thermostatic valve inserts (ranging from 40°C to 80°C thresholds), blow-down intake regulators, and electronic solenoid valves matching OEM calibration curves.
Each unit is bench-tested against pressurized thermal cycle chambers to eliminate valve stickiness, oil emulsification during low-load intervals, and sudden pressure drops during sudden plant demand surges.
Why Sourcing Atlas Compressor Parts from China Outperforms Global Rivals
China's industrial clustering has transformed aftermarket pneumatic equipment manufacturing from a low-cost substitute into a technologically advanced, highly competitive global engineering hub.
Full Supply-Chain Integration
From metallurgical casting in precision grey iron and nodular iron to automated 5-axis CNC machining centers, China concentrates entire component ecosystems within dedicated machinery clusters. This eliminates geographic latency, minimizes raw material handling overheads, and provides immediate raw stock availability even during global commodity disruptions.
Strict Quality Verification (ISO & CE)
Every batch of replacement parts undergoes coordinate measuring machine (CMM) dimensional verification, dynamic rotor balancing according to ISO 1940 Grade G2.5, hydrostatic pressure testing up to 25 bar for oil coolers and coolers, and thermal stability audits. This eliminates the uncertainty historically associated with third-party consumables.
Economies of Scale & Fast Turnaround
Chinese production lines produce millions of filter cartridges, sensor kits, and thermodynamic couplings annually for both domestic and international markets. Large-volume production scales down unit costs significantly, allowing international procurement departments to acquire Tier-1 level components at wholesale factory rates.
| Component Group | OEM Standard Reference | China Aftermarket High-Spec Equivalent | Comparative Lifespan | Procurement Cost Advantage |
|---|---|---|---|---|
| Screw Airend Overhaul Kits | Pre-packaged OEM Bearings & PTFE Lip Seals | SKF/FAG Angular Contact Bearings + Fluororubber Oil Seals | 35,000 – 45,000 Hours | 50% – 65% Savings |
| Air / Oil Separator Elements | OEM Micro-Glass Fiber Wrap | Ahlstrom / HV Synthetic Borosilicate Nano-Media | 4,000 – 6,000 Hours | 45% – 60% Savings |
| Synthetic Compressor Lubricants | Roto-Inject Fluid / Roto-Xtend Duty | Fully Formulated PAO / POE Ester Synthetic Base Stocks | 8,000 – 12,000 Hours | 40% – 55% Savings |
| Thermostatic & MPV Valve Kits | Brass Casting Assembly Kits | Forged Brass & Hard-Anodized Aluminum + Viton O-Rings | 8,000 Hours / 2 Years | 50% – 70% Savings |
| Air Intake & Oil Filter Kits | Cellulose Core Filters | Flame-Retardant Nano-Coated Cellulose / Microfiber | 3,000 – 4,000 Hours | 55% – 75% Savings |
Technological Evolution & Future Trends in Industrial Compressed Air
The global industrial compressed air market is transitioning rapidly toward energy decarbonization, real-time IoT monitoring, and preventive lifecycle asset management.
IoT-Enabled Predictive Telematics
Modern compressor installations are discarding rigid hour-meter maintenance schedules. With smart sensor integration, differential pressure transducers, vibration spectral sensors, and real-time lubricant dielectric sensors upload operational telemetry to cloud monitoring systems. Maintenance teams can predict separator saturation or bearing spalling weeks before failure occurs.
Variable Speed Drive (VSD) Retrofits
With electricity accounting for roughly 75% of a compressor's total 10-year operating cost, retrofitting fixed-speed screw compressors with high-efficiency frequency inverters (VFD) and permanent magnet (PM) motors saves between 20% to 35% in energy. Modern aftermarket controllers allow seamless variable-speed synchronization across multi-compressor networks.
Zero-Carbon Heat Recovery Systems
Up to 90% of electrical energy consumed by a rotary screw compressor is converted into heat. Cutting-edge industrial facilities integrate modular aftermarket plate heat exchangers directly into the internal oil circulation circuit. This allows plants to capture thermal energy for boiler feed-water preheating, space heating, and clean process hot water without extra fuel.
Mission-Critical Applications & Heavy Industry Solutions
Reliable compressed air is known as the "Fourth Utility" in modern production facilities. Here is how specialized component engineering supports heavy manufacturing environments.
Automotive & High-Speed Robotics
Automated automotive assembly plants require continuous pneumatic line pressure for robotic welding, paint spray booths, and transfer presses. A 0.5 bar pressure drop can halt an entire production line. Our heavy-duty air-oil separators and rapid-response intake valves ensure consistent volumetric delivery, while paired diesel gensets guarantee zero line halts during local grid fluctuations.
Petrochemical & Hazardous Refining
Petrochemical facilities demand intrinsically safe operation, anti-static grounding copper wire in separators, and spark-free component metallurgy. Our components are manufactured to withstand aggressive hydrocarbon vapors, elevated ambient temperatures, and 24/7 continuous duty cycles without diaphragm embrittlement or seal leaks.
Food, Beverage & Pharmaceuticals
Where compressed air comes into direct or indirect product contact, zero oil aerosol contamination is mandatory. We provide Class 0 oil-free compressor replacement parts, food-grade synthetic lubricants conforming to NSF H1 specifications, and sterile stainless-steel terminal particulate filter elements.
Global Enterprise Sourcing & Inventory Risk Mitigation
A strategic framework tailored for plant engineering managers, regional distributors, and EPC contractors seeking predictable lead times, audit-ready compliance, and resilient component pipelines.
Customized VMI & Consignment Buffer
Unplanned compressor stoppages cause thousands of dollars in lost industrial output per hour. We partner with multinational enterprises to structure Vendor-Managed Inventory (VMI) arrangements, holding critical wear kits, complete spare airends, and electrical sensor packages in bonded export warehouses for same-week dispatch.
Custom OEM/ODM Branding & Packaging
For industrial machinery service providers and compressed air distributors worldwide, we offer complete white-label manufacturing services. This includes customized laser etching of customer part numbers, custom packaging, localized manuals, and tailored performance warranties backed by our factory engineering division.
Multi-Modal Logistics & Trade Compliance
From sea freight (FCL/LCL) through major coastal hubs like Tianjin, Qingdao, and Shanghai to expedited DHL/FedEx air freight for emergency plant repairs, our dedicated documentation team guarantees complete compliance with origin declarations, Certificate of Origin (CO), Form E/A, and dual-use customs clearance documentation.
Precision Component Engineering Matrix for Screw Compressors
A systematic technical overview of essential replacement components, wear patterns, and manufacturing quality controls required to preserve Atlas Copco compatible machine integrity.
Air-Oil Separation Media
Separation media efficiency directly controls plant operating costs. Our spin-on and drop-in separator canisters feature multi-layer wrapped borosilicate nano-fibers. High-integrity electro-conductive grounding tabs prevent static discharge sparks within the oil vessel, delivering safety and regulatory compliance.
Intake Unloader & Blowdown Valves
Modulating intake valves control the compressor's transition between loaded, partially loaded, and unloaded states. Constructed from aerospace-grade cast aluminum alloys with fluorocarbon seals, our valves resist varnish buildup and eliminate delayed unloading cycles that waste electrical energy.
Plate-Fin Heat Exchangers & Coolers
High discharge temperatures cause automatic machine shutdowns and accelerate oil breakdown. Our vacuum-brazed aluminum plate-fin oil coolers and aftercoolers deliver up to 30% superior thermal transfer compared to conventional tube bundles, engineered to operate smoothly up to 50°C (122°F) ambient environments.
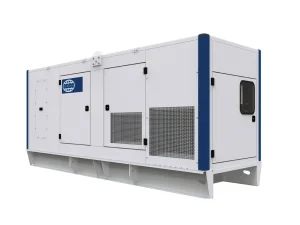
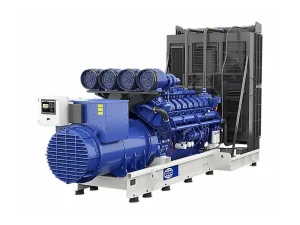
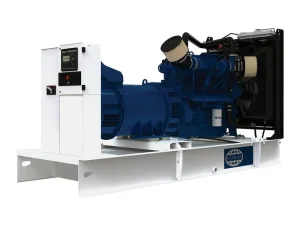
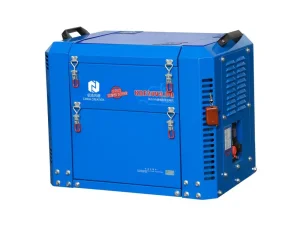
Continuous Power & Heavy-Duty Compressor Auxiliary Units
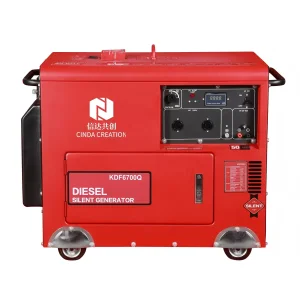
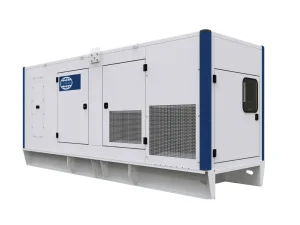
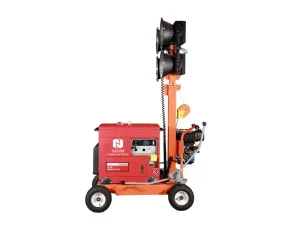
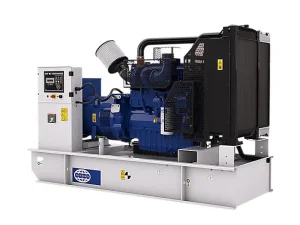
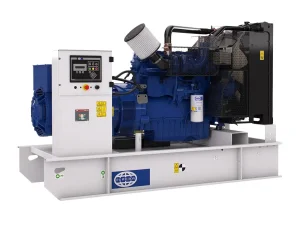
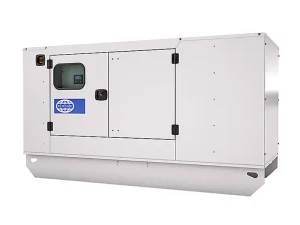
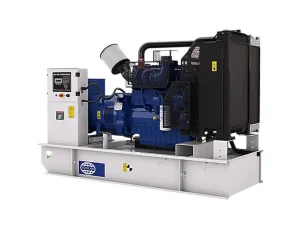
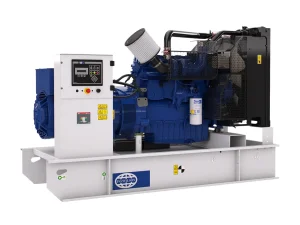
Complete your facility's reliability architecture with our full series of heavy-duty industrial diesel generator systems, Perkins-powered prime gen-sets, and low-noise emergency equipment.
Frequently Asked Questions on Atlas Compressor Parts Procurement
Comprehensive engineering clarifications addressing cross-compatibility, material specifications, warranty terms, and international B2B shipping logistics.
Are aftermarket Atlas Copco parts 100% interchangeable with genuine OEM units?
Yes. Our alternative replacement parts are reverse-engineered directly from authentic OEM specifications utilizing 3D coordinate measuring machines (CMM) and dynamic flow bench tests. Mounting flange dimensions, thread pitches (BSP/NPT), seal seats, and differential pressure characteristics match Atlas Copco original equipment (such as GA11, GA22, GA37, GA75, GA160, and GX series) precisely, ensuring seamless drop-in replacement without field modification.
How does the filtration efficiency of Chinese aftermarket air/oil filters compare to OEM?
We utilize the exact same specialized media sourced from world-renowned filtration media producers, including Hollingsworth & Vose (USA) and Ahlstrom (Finland). Our air intake filters achieve 99.9% filtration at 1-3 microns. Our oil filters incorporate high-burst-pressure steel housings and bypass valves calibrated to OEM specs. Our oil separators maintain downstream residual oil carryover below 3 ppm across their rated 4,000-hour service life.
What warranty protection is provided for rebuilt screw airends and mechanical parts?
All complete replacement screw air ends and major mechanical assemblies (coolers, gear sets, shaft assemblies) carry a comprehensive 12-month factory warranty counted from commissioning, or up to 18 months from the bill of lading date. Consumable service kits (filters, separator elements, synthetic lubricants) are guaranteed against manufacturing defects for their standard operational design life when operated under normal industrial ambient parameters.
Can synthetic compressor oils be safely mixed with existing Roto-Inject or Roto-Xtend fluids?
While our synthetic polyalphaolefin (PAO) and synthetic ester base lubricants are chemically formulated to be compatible with standard OEM polyol-ester and hydrocarbon compressor fluids, we strongly recommend a full flush procedure during oil changeovers. Flushing prevents additive precipitation, guarantees peak demulsibility (water separation), and ensures full 8,000+ hour oxidation stability without varnish buildup.
What documentation is required to verify the exact part numbers for legacy or customized compressors?
To ensure 100% component compatibility, buyers simply need to provide the compressor serial plate photo showing the Model Designation, Serial Number (AIF/APF/ARP sequence), and Operating Pressure. If the original data plate is missing, sharing the existing component part number stamped into the filter canister, casting body, or electronic sensor will allow our application engineers to cross-reference our internal database of over 120,000 industrial part numbers within minutes.
How are orders packaged to protect precision rotors and coolers during ocean transit?
All precision machined components, including rotor assemblies and shafts, are treated with vapor corrosion inhibitor (VCI) anti-rust coatings, vacuum-sealed in heavy-duty polyethylene barrier bags, and secured within custom foam-lined, export-grade ISPM-15 fumigated wooden crates. Fragile aluminum plate-fin coolers are cushioned with high-density expanded polyurethane to eliminate fin distortion or seam cracking from shipping vibrations.