Featured Industrial Power & Piston-Driven Generator Sets
Engineered for seamless integration with Perkins, Weichai, and FG Wilson powertrain architectures. Every unit is dynamically pre-tested for optimal cylinder pressure and peak thermal efficiency before global dispatch.
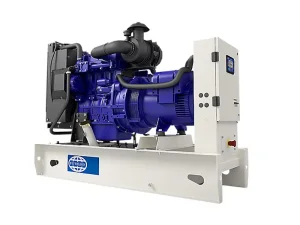
China Wilson Open Type Small Diesel Generator Sets 230 V, 50 Hz P16-1
Configure & Procure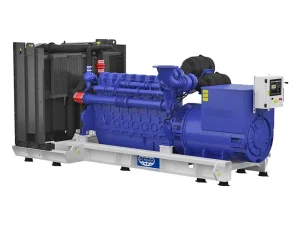
High-Quality Large Range >800 kVA FG Wilson Diesel Generator P1000-1
Configure & Procure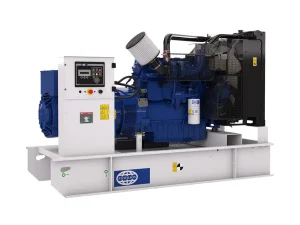
China Medium Range 225-938KVA High Efficiency Diesel Generator Set P313-5
Configure & Procure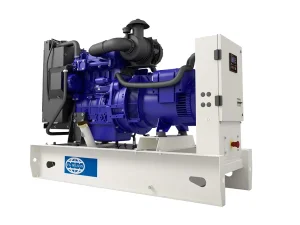
China Wilson Silent Type Small Diesel Generator Sets 400/230 V Standby 9.5kVA P9.5-4
Configure & Procure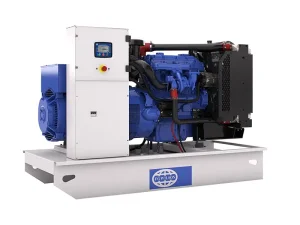
High-Quality Wilson Open Type Small Diesel Generator Sets 400/230 V P88-3
Configure & Procure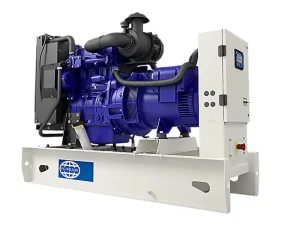
High-Quality FG Wilson Low Noise Energy Solution Generator Sets P11-6S
Configure & Procure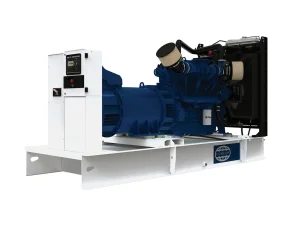
China Medium Range 225–938 kVA FG Wilson Generator Set P688-3
Configure & Procure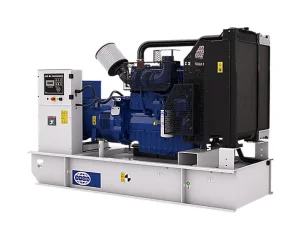
China FG Wilson P400-3 Generator Set Medium Range 225-938 kVA
Configure & ProcureDemystifying the "Cheap" Paradigm: High-Precision Metallurgy vs. Total Cost of Ownership
In modern heavy-duty internal combustion engines, cylinder liner and piston kits operate at the nexus of peak thermal flux, micro-frictional wear, and extreme mechanical pressures exceeding 220 bar.
In the global power equipment aftermarket and OEM manufacturing sectors, the term "cheap cylinder liner pistons exporters" has historically carried conflicting interpretations. For procurement managers and fleet maintenance directors, "cheap" was often synonymous with elevated scuffing risks, premature ring blow-by, and inconsistent metallurgical graphite nodularity. However, across modern Industry 4.0 production hubs in China, technological convergence has fundamentally redefined this dynamic.
Today, achieving cost leadership is not about sacrificing alloy purity or dimensional tolerances; it is the structural result of automated centrifugal casting, closed-loop CNC plateau honing, and hyper-efficient multi-tiered supply chain clusters. At Beijing Xinda Creation Machinery Equipment Co., Ltd. (Cinda Creation), our engineering workflows integrate raw-material bulk sourcing with precision machining lines to deliver heavy-duty cylinder liner and piston components at factory-direct pricing—reducing unit acquisition costs by 30% to 48% while maintaining full compliance with strict European and American combustion standards.
Key Metallurgical Trends Shaping Cylinder Liner & Piston Evolution
Industrial internal combustion engines—ranging from small-range generator sets (<220 kVA) to mission-critical multi-megawatt systems (>800 kVA)—face unprecedented operational demands due to high-pressure common rail (HPCR) injection, aggressive exhaust gas recirculation (EGR), and the transition toward alternative fuels (hydrogen blending, methanol, and high-ethane natural gas). This requires rapid advances in cylinder kit materials:
Centrifugal Vermicular & Boron Cast Iron
Modern wet and dry cylinder liners feature centrifugal casting with controlled boron (0.05-0.12%) and phosphorus contents. This creates a hard, wear-resistant phosphide eutectic network within a pearlitic matrix, preventing bore polishing and minimizing frictional scuffing under elevated BMEP (Brake Mean Effective Pressure).
Hypereutectic Silicon Alloys & Steel Crowns
For high-load genset engines (such as the FG Wilson P1000-1 and P1375-1 series), monobloc pistons are replaced by hypereutectic aluminum skirts paired with forged steel crowns. Laser-welded internal cooling galleries allow oil jets to reduce top ring land temperatures by more than 40°C.
Advanced Tribological Coatings (PVD & MoS2)
Piston skirts are screen-printed with molybdenum disulfide (MoS2) and graphite polymers to reduce hydrodynamic friction during cold starts. Compression rings are upgraded with Physical Vapor Deposition (PVD) chromium nitride (CrN) or Diamond-Like Carbon (DLC) for minimal bore wear.
B2B Sourcing Analysis: Western OEM vs. Uncertified Copy vs. Advanced Factory 4.0 Exporter
Evaluate the technical, operational, and financial trade-offs between traditional brand-name distributors, non-certified gray market suppliers, and ISO-audited Chinese engineering exporters.
| Evaluation Parameter | Western OEM Brands | Unregulated "Low-Bid" Workshops | Cinda Creation / Factory 4.0 Exporter |
|---|---|---|---|
| Bore Honing Geometry | Plateau cross-hatch (35°–45° angle, Rk < 0.4µm) | Inconsistent rotary hone, high peak roughness | CNC Plateau Honed (38° Angle, Rpk/Rvk Calibrated) |
| Cylinder Liner Metallurgy | Pearlitic matrix, vermicular boron iron | Scrap gray iron, uncontrolled flake graphite | Centrifugal Cast Boron-Copper Alloy (ISO Verified) |
| Piston Thermal Profiling | Integrated cooling galleries, high Si content | Solid cast, no gallery, thermal cracking risk | Laser-Welded Gallery / Steel Crown Options |
| Unit Acquisition Cost | 300% – 500% Markup (Brand Premium) | Lowest Initial Cost (High Risk) | Direct Factory Economics (40-60% Savings) |
| Expected Service Life | 15,000 – 20,000 Hours (Baseload) | < 3,000 Hours (Early Cavitation Failure) | 12,000 – 18,000 Hours (Fully Documented) |
| Quality Assurance & Auditing | Global ISO & Lloyd's Type Approval | No traceable test bench certification | ISO 9001, 14001, 45001 + 100% Coordinate CMM |
China Factory 4.0: Automated Scale, Supply Chain Agility & Global Logistics
Operating from Tongzhou District, Beijing, our manufacturing integration unites raw-material smelting, ultra-precision automated tooling, and rapid containerized export logistics for global B2B clients.
The core structural advantage of procuring cylinder liners, pistons, and complete generator systems from China lies in regional industrial clustering. Within integrated supply corridors, casting foundries, CNC machining facilities, heat treatment plants, and surface finishing lines operate in tight geographic coordination. This localized integration eliminates intermediate shipping delays, reduces production bottlenecks, and enables tight quality controls across every stage of fabrication.
At Cinda Creation, our manufacturing partners employ multi-axis German and Japanese CNC transfer lines with automated tool-wear compensation. Cylinder liners are finished with robotic diamond plateau honing brushes to produce precise oil retention valleys (cross-hatch angle 38° ± 2°), eliminating the typical 100-hour engine break-in period and preventing early cylinder glazing. Pistons undergo 100% non-destructive ultrasonic testing to verify internal cooling gallery integrity, followed by automated optical scanning for 5-axis pin bore alignment.
Optical Spectrum Assay
Every melt batch undergoes direct-reading spectrometer analysis to verify trace elements (B, Cu, Cr, Mo) for uniform pearlite structure and graphite flake distribution.
Sub-Micron Metrology
Zeiss 3D Coordinate Measuring Machines (CMM) inspect piston skirt ovality, barrel profiles, and wrist pin bore clearances down to ±0.0015 mm tolerances.
Anti-Cavitation Passivation
Outer diameters of wet liners receive specialized phosphate coatings and induction surface hardening to resist high-frequency coolant cavitation shockwaves.
Export-Grade Packaging
VCI (Vapor Corrosion Inhibitor) heat-sealed encapsulation combined with reinforced multi-layer honeycomb cartons prevents maritime oxidation during overseas transit.
Localized Application Scenarios: High Ambient, Sub-Zero & Mission-Critical
Engine components and generator sets from Cinda Creation are deployed across challenging operating environments worldwide, maintaining steady power and high wear resistance.
Long-Distance Pipeline Pumping
On the 2,400-kilometer China–Myanmar crude oil pipeline, continuous prime-duty power is sustained by 17 natural gas units and 5 heavy diesel generator sets. These systems run uninterrupted for months, relying on precision cylinder-piston clearances to prevent thermal oil blow-by.
Arctic & Cold Weather Sites
Our FG Wilson and Perkins-powered configurations have operated in extreme sub-zero conditions (-40°C) for over 20 years. Matched thermal expansion coefficients between pistons and liners prevent cold-start scuffing and maintain full cylinder compression in deep freeze environments.
High-Ambient Desert Enclosures
In Middle Eastern and tropical facilities where ambient temperatures exceed 50°C, custom acoustic canopies and high-heat piston alloy formulations prevent thermal crown deformation, ensuring continuous prime power without premature engine derating.
Hospital & Emergency Microgrids
From rural clinics to international hub projects—such as emergency construction power for an Ethiopian airport terminal—our silent gensets feature ATS automation to achieve full voltage and frequency stability in under 10 seconds during main utility dropouts.
Frequently Asked Technical Questions
Direct answers to the common technical and supply chain inquiries submitted by fleet mechanics, power station operators, and global overhaul contractors.
How does Cinda Creation ensure low prices on cylinder liners and pistons without cutting quality?
What specific hone angle and surface parameters are applied to your cylinder liners?
What is the functional difference between Prime Power and Standby Power in generator ratings?
How do you combat wet cylinder liner cavitation erosion in high-output engines?
Can your Perkins generator parts and cylinder components match existing engine serial numbers?
What warranty and after-sales terms protect global buyers?
Heavy Power Units, Silent Enclosures & Overhaul Assemblies
Explore the balance of our core dispatch units, spanning silent urban enclosures, open frame plant configurations, and high-output prime diesel generation systems.
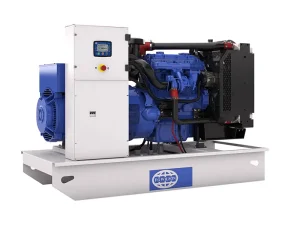
China Wilson 110KVA Portable Diesel Generator P110-3
Configure & Procure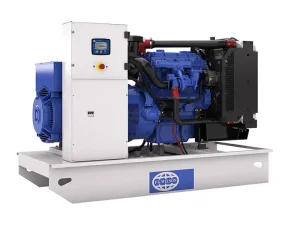
Cheap Wilson 90KVA Industrial Power Generator P90-3S
Configure & Procure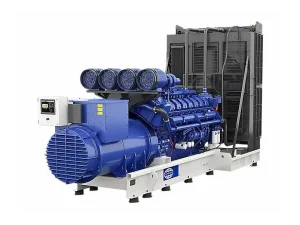
High-Quality Large Range >800 kVA FG Wilson Generator P2000-3
Configure & Procure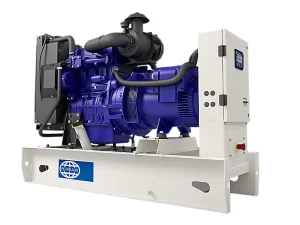
High-Quality Wilson Small Range <220 kVA Silent Generator P12-1S
Configure & Procure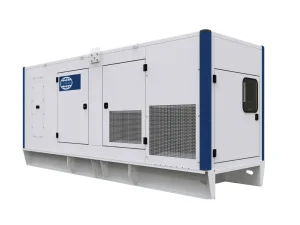
Cheap FG Wilson Generator Set 225-938KVA Low Noise P750-3
Configure & Procure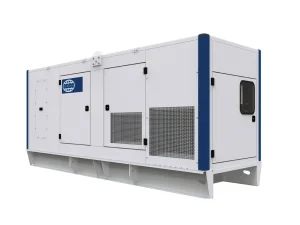
Cheap FG Wilson High-Performance Generator P850-1
Configure & Procure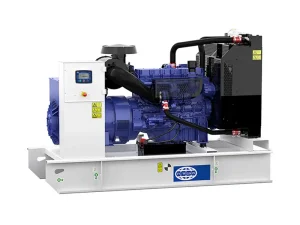
High-Quality Wilson Open Type Small Diesel Generator P150-5
Configure & Procure
Cheap Wilson Open Type Small Diesel Generator Sets P26-6S
Configure & ProcureRequest Factory-Direct Quotations & Technical Spec Sheets
Supply us with your required cylinder liner bore diameters, piston crown geometry, or complete generator model ratings. Our Beijing-based engineering team configures, validates, and packages your order within 24 business hours.