Specified Prime & Standby Heavy-Duty Power Equipment
Explore precision-configured diesel generators, industrial prime-movers, and heavy-duty powertrain assemblies built for demanding operating envelopes worldwide.
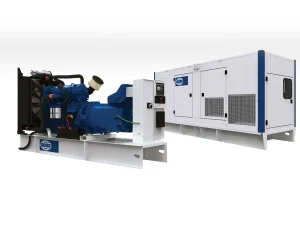
China FG Wilson Open Type Medium Diesel Generator Sets P501-3 Supplier, Service
View Product Specs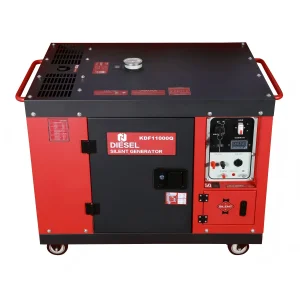
Cheap Powerful silent small diesel generator sets Low Noise for Camping and Home Suppliers, Exporter
View Product Specs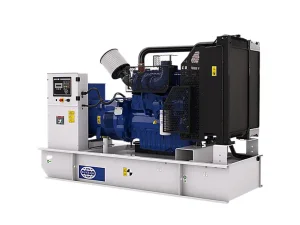
China FG Wilson Generator set 225-938kVA, Industrial-Grade Power Guarantee P300-5 Suppliers, Service
View Product Specs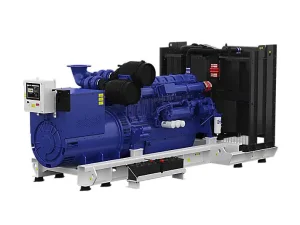
Cheap Large 1125 kVA Versatile Generators for Large-Scale Power Needs P1250-1 Exporter, Service
View Product Specs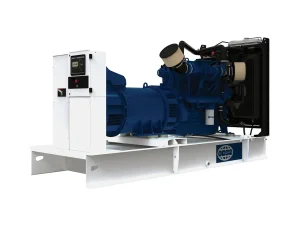
High-Quality Fg Wilson 225-938KVA High Efficiency Diesel Generator Set P605-3 Suppliers, Service
View Product Specs
High-Quality Versatile and Powerful Portable Silent Generator Set KDF11000Q Supplier, Suppliers
View Product Specs
High-Quality 6.6kVA 8KW Silent Diesel Generator Set Diesel Engine with Soundproof Enclosure Supplier, Service
View Product Specs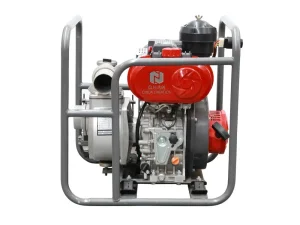
Cheap High-Performance High-Pressure Air-cooled Diesel Engine KD7 Supplier, Exporters
View Product SpecsThe Strategic Role of Precision Camshaft Engineering in Heavy-Duty Powertrains
Within modern high-efficiency internal combustion engines, heavy-duty industrial diesel gen-sets (such as FG Wilson and Weichai configurations), and continuous-duty marine propulsion systems, the camshaft serves as the fundamental mechanical brain of thermal efficiency and gas exchange dynamics.
Tasked with dictating valve opening profiles, variable valve timing (VVT), valve duration, and lift velocity against extreme contact pressures, an inferior camshaft induces valvetrain harmonics, accelerated lobe scuffing, parasitic pumping losses, and catastrophic catastrophic timing chain or geartrain failure. For mission-critical infrastructure—from hospital emergency standby power plants to remote Arctic oil pipelines—specifying high-integrity camshaft components manufactured to sub-micron geometric tolerances is an engineering necessity, not an optional upgrade.
Partnering with accredited Chinese manufacturing specialists empowers global enterprises to leverage advanced metallurgy—including chilled ductile cast iron, induction-hardened forged alloy steel (such as 42CrMo4 and EN40B), and hollow assembled camshaft architectures—delivering optimal strength-to-weight ratios and verified lifecycle reliability.
| Engineering Metric | Standard Commercial Grade | High-Quality Exporter Grade |
|---|---|---|
| Lobe Profile Tolerance | ±0.025 mm | ±0.002 mm (CNC Super-finish) |
| Surface Hardness | HRC 48 - 52 | HRC 58 - 64 (Induction/Nitrided) |
| Surface Roughness (Ra) | Ra 0.40 - 0.60 µm | Ra ≤ 0.15 µm (Micro-honed / DLC) |
| Concentricity & Runout | 0.030 mm TIR | ≤ 0.008 mm TIR Total Indicator |
| Base Material Options | Gray Cast Iron / C45 | Chilled Ductile Iron / Forged 42CrMo |
| Non-Destructive Testing | Random Batch Visual | 100% Eddy Current & Mag Particle |
Global Enterprise Procurement Needs: What Tier-1 Buyers Demand
Procuring camshaft assemblies for heavy commercial fleets, stationary power plants, and marine diesel platforms requires balancing tribological resilience, lead-time predictability, and auditable pedigree.
Tribological Metallurgy & Material Integrity
Global OEMs demand verified carbon-microstructure distribution. Whether executing chill casting to produce white iron cam lobes with pearlite cores or forging high-tensile 42CrMo alloy, the core must retain cyclic impact ductility while the skin resists rolling-sliding Hertzian fatigue stress up to 1,500 MPa.
Sub-Micron Profile Repeatability
Modern emissions regulations (Euro VI and EPA Tier 4 Final) dictate sub-micron cam lobe lift and acceleration curves. Procurement teams specify multi-axis Landis or Schaudt CNC cam grinders and Adcole optical inspection systems to verify lobe shape angularity within seconds of arc.
Full-Traceability Quality Audits
Corporate procurement contracts enforce IATF 16949-grade lot tracking. Every single camshaft shipped internationally must link back to optical spectrometer melt analysis, heat-treatment furnace thermocouple records, non-destructive crack testing, and dimensional CMM inspection data packs.
Chinese Factory Supply Chain Advantages in Precision Camshaft Production
China's comprehensive manufacturing ecosystem delivers high-volume scalability, agile customization, and unrivaled cost-to-performance ratios for global powertrain distributors.
End-to-End Vertical Integration
From automated cupola foundry casting and sand-core reclamation to precision rough turning, induction heat treatment, and finish grinding, Chinese plants consolidate all production tiers under one roof, cutting intermediate logistics cycles by 40%.
Advanced Induction Hardening Cells
Utilizing computerized medium-to-high frequency CNC scanning induction equipment, our partner facilities achieve uniform case hardening depth (3.0 mm to 5.0 mm) with zero decarburization, ensuring high wear resistance across extreme operational life spans.
Economies of Scale & Raw Material Access
Close proximity to leading domestic metallurgical centers guarantees immediate availability of certified alloy steels (40Cr, 42CrMo, 20CrMnTi) and high-purity nodular pig iron, insulating international clients from global raw-material price volatility.
Agile OEM & Aftermarket Tooling
Rapid in-house CNC pattern and mold fabrication reduces new camshaft prototyping timelines from standard 16-week Western lead times down to under 28 calendar days, accompanied by complete PPAP Level 3 technical documentation.
Localized Engineering Support & Rigorous Compliance Assurance
International industrial buyers cannot afford cross-border friction when dealing with mission-critical powertrain components. Our strategic operational model eliminates time-zone barriers and provides ironclad compliance for overseas projects.
Through our dedicated Beijing engineering headquarters (Beijing Xinda Creation Machinery Equipment Co., Ltd.), we manage bilingual technical communication, finite element simulation (FEA) reviews, and warranty commitments backed by our standardized 12-month operational warranty and 24-hour response protocol.
We ensure that every exported camshaft, engine assembly, and replacement valvetrain component adheres strictly to target destination regulatory mandates:
- EU Machinery Directive 2006/42/EC & CE Certification for all integrated motorized gensets and engine packages.
- ISO 9001, ISO 14001, and ISO 45001 audited management processes across casting, machining, packing, and dispatch.
- RoHS & REACH Compliance verifying that surface anti-corrosion oils and phosphate coatings are 100% free of hazardous heavy metals.
- Standardized Export Packaging utilizing VCI anti-corrosion barrier wrapping, custom vapor-proof desiccants, and heat-treated ISPM-15 compliant sea-freight crates.
Standardized Quality Assurance Audit Protocol
Stage 1: Spectrometric Chemical Validation — Every heat melt is verified via spark emission spectrometry to guarantee precise Cr, Mo, Ni, and V carbon-equivalent ratios.
Stage 2: Ultrasonic Sub-surface Screening — Full-length volumetric screening to eliminate internal micro-shrinkage porosity in chill-cast and forged billets.
Stage 3: Automated Lobe Profile Tracing — Continuous CNC optical tracing comparing theoretical polynomial lift curves against actual ground surfaces.
Stage 4: Barkhausen Noise Analysis — Sensitive magnetic non-destructive testing to detect thermal grinding burns or micro-cracking prior to final preservation packing.
Real-World Deployment Scenarios & Heavy-Duty Operating Environments
Camshafts engineered by high-caliber manufacturers operate under vastly divergent thermal and mechanical duty cycles across the globe.
Continuous Prime & Standby Gensets
In stationary power stations utilizing FG Wilson and Perkins platform architectures (from 110 kVA up to 1375 kVA), camshafts must sustain uninterrupted 1,500 rpm or 1,800 rpm synchronous speeds without frequency flutter, guaranteeing instant torque response upon sudden step-load transients.
High-Torque Marine Propulsion & Pumping
Working in corrosive salt-air environments and subject to extreme torsional vibration, our marine-grade camshafts feature phosphate passivated bearing journals and induction-hardened fuel-injection lobes engineered to actuate high-pressure mechanical unit injectors (MUI) under continuous sea loads.
Extreme Sub-Zero & Desert Mining Fleets
Proven in field applications spanning from minus 40°C Siberian and Arctic energy operations to 55°C Middle Eastern pipeline pumping stations. Specialized metallurgical grain refinement prevents low-temperature embrittlement while maintaining lubricating oil-film retention in extreme heat.
Industry Trends: The Future of Camshaft & Valvetrain Engineering
As the international automotive and heavy machinery sectors transition toward decarbonization, high-efficiency combustion, and hybrid-powertrains, camshaft design is undergoing fundamental technical transformations.
Assembled Lightweight Camshafts
Replacing traditional monolithic cast iron shafts, assembled camshafts utilize precision hollow steel tubes with individually hydroformed or thermal-shrink fitted sintered metal lobes. This reduces rotating valvetrain inertia by 30% to 45%, directly cutting parasitic drive torque and lowering specific fuel consumption.
Variable Valve Actuation & Cylinder Deactivation
Modern diesel and natural gas powerplants integrate multi-profile sliding camshaft segments (e-Cam / VVA) that shift axially via electromagnetic actuators. This enables dynamic cylinder deactivation (CDA) during light load cycles, raising exhaust temps for SCR aftertreatment while slashing CO2 and NOx emissions.
Hydrogen & Methanol Combustion Profiles
Zero-carbon fuels exhibit completely different flame speeds, cylinder pressures, and lubricity characteristics. Forward-thinking manufacturers are engineering specialized asymmetric lobe profiles with Diamond-Like Carbon (DLC) nanocomposite coatings to survive dry, zero-sulfur combustion environments.
Enterprise Buyer’s Checklist: Optimizing Total Cost of Ownership (TCO)
Purchasing agents often make the mistake of evaluating camshaft procurement purely on initial per-unit FOB quotation. A true Total Cost of Ownership evaluation examines lifetime reliability, installation downtime risk, and warranty backing.
1. In-Process Heat Treatment Control
Verify whether the manufacturer employs computerized batch tracking with automated quench immersion. Inadequate quenching produces retained austenite, resulting in progressive dimensional swelling and binding within the engine block tunnel during operation.
2. Dynamic Balancing & Geartrain Fit
Specify maximum residual dynamic unbalance standards (ISO 1940 Grade G6.3 or G2.5). Unbalanced camshafts introduce high-frequency torsional oscillations that shear gear retaining bolts, shatter drive dampers, and prematurely wear valve stem guides.
3. Preservation & Seaworthy Logistics
Camshaft ground finishes are vulnerable to atmospheric oxidation during trans-oceanic freight. Insist on immersion-applied neutral pH rust-preventative oil, individual anti-static VCI sleeves, and shock-cushioned multi-compartment timber crating.
Frequently Asked Questions: Powertrain & Valvetrain Procurement
Comprehensive technical guidance addressing common engineering queries encountered by global fleet managers, OEM contractors, and plant engineers.
What material is best suited for heavy-duty commercial diesel camshafts: chilled cast iron or forged steel?
How does camshaft lobe wear directly impact generator output and fuel consumption?
What quality documentation and testing reports should accompany overseas camshaft shipments?
Can Beijing Xinda Creation supply custom or obsolete camshafts based on physical samples or engineering drawings?
What after-sales warranty coverage and international technical support do you provide?
Commercial Power Solutions, Diesel Engines & Auxiliary Units
Browse our integrated inventory of silent acoustic units, open-frame installations, single-cylinder utility engines, and heavy industrial gen-sets ready for global dispatch.
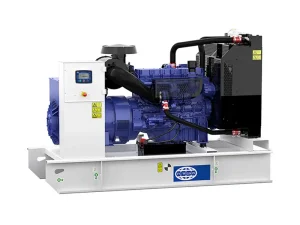
China FG Wilson Generator Sets Power You Can Trust Small Type P200-3 Supplier, Service
View Product Specs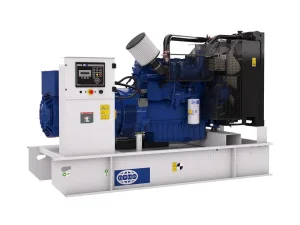
High-Quality FG Wilson 225-938kVA High-Efficiency Generator Set, Stable Power Supply Solution P275-2 Supplier, Exporters
View Product Specs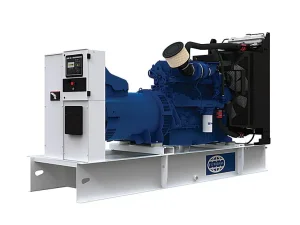
Cheap Medium Range 225 – 938 kVA Generator Set P450-2 Supplier, Exporter
View Product Specs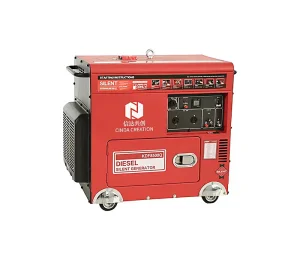
High-Quality Quiet 7.5KVA Diesel Generator Reliable Power Minimal Noise for Building Backup Power Exporter, Service
View Product Specs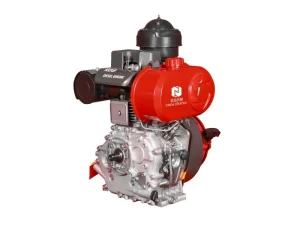
Cheap Single Cylinder Air-cooled Diesel Generator KD9 Supplier, Exporter
View Product Specs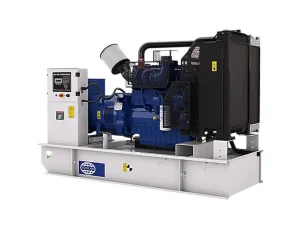
Cheap Medimu Range 225-938KVA Fg Wilson Industrial-Grade Generator Set P330-5 Exporter, Service
View Product Specs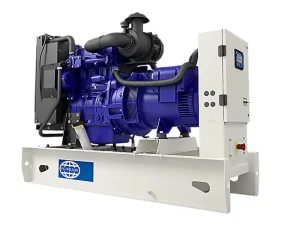
High-Quality FG Wilson Low Noise Energy Solution Generator Sets P11-6S Suppliers, Exporter
View Product Specs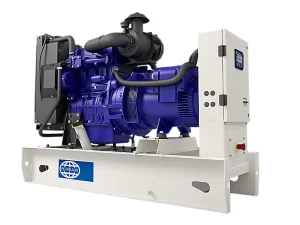
High-Quality Wilson Small Range <220 kVA Silent Power Generator P12-1S Exporter, Service
View Product SpecsConnect Directly with Our Powertrain Sourcing Engineers
Submit your 2D/3D part prints, engine application profiles, or project equipment specifications. Receive comprehensive DFM analysis, metallographic recommendations, and certified FOB/CIF export pricing within 24 hours.